Garage Openers - PFC CONTROLS | Miami, Gate Operators, Sliding Gate, Swing Gate, Intercoms, Turnstiles, Bollards, Barrier gate

MENU
Go to content

Why Choose Swiss Turning Services for Titanium Bone Screws?

Swiss Turning Services For Titanium Bone Screws offer a practical route to producing precise, dependable orthopedic components. Titanium is lightweight, corrosion resistant, and compatible with many clinical applications. However, its strength can make machining demanding. Heat buildup, tool wear, and burr formation require careful control. Experienced Swiss machining teams understand these challenges through repeated production work.

Swiss-type lathes support stable cutting and accurate miniature features. They can maintain tight relationships between threads, drive recesses, and screw bodies. This matters when a bone screw must fit consistently with related surgical instruments. Skilled operators also monitor surface finish, dimensional results, and material traceability. Reliable suppliers use documented inspections, calibrated equipment, and controlled production procedures. These practices support quality expectations within regulated medical device manufacturing.

Tiny details matter. A clean thread crest can influence assembly performance. A small burr may create an avoidable concern. No machining process is flawless, and every supplier deserves careful evaluation. Buyers should review experience with implant-grade titanium, inspection records, process validation, and corrective-action practices. Certifications can support confidence, but they never replace technical questions. Clear communication remains essential when specifications change or tolerances become difficult. The strongest partnership combines advanced equipment with accountable engineering judgment. That balance helps manufacturers pursue consistent titanium bone screw production without overlooking practical risks.

Why Choose Swiss Turning Services for Titanium Bone Screws?

Titanium Bone Screws: Materials, Uses, and Performance Requirements

Titanium bone screws combine low density, corrosion resistance, and strong biological tolerance. Titanium alloy Ti-6Al-4V has a density near 4.43 g/cm³ and an elastic modulus around 110 GPa. These values support lighter implants with useful mechanical strength. ASTM F136 and ISO 5832-3 define key requirements for implant-grade titanium alloys. Material certificates must confirm chemistry, heat treatment, and traceability. Small deviations matter.

Bone screws support fracture fixation, spinal stabilization, and reconstructive procedures. Thread geometry must provide reliable purchase without excessive insertion torque. Surface roughness also affects cleaning, coating, and tissue response. The World Health Organization reported that 1.71 billion people live with musculoskeletal conditions. Demand is substantial, but volume must never replace control.

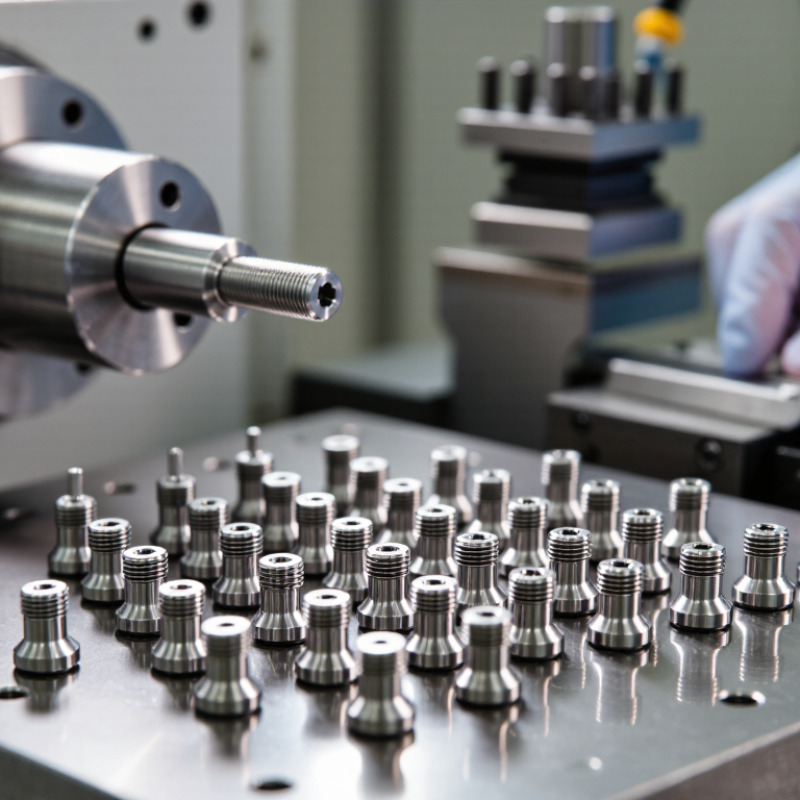
Swiss turning is useful for miniature titanium screws. A guide bushing supports slender bars during machining. This can improve concentricity across the thread, shank, and drive recess. Live tooling can produce precise slots or hexalobular features in one setup. Coolant delivery and sharp tooling help reduce heat and burr formation. However, machining is not automatically perfect. Tool wear may change thread pitch or crest form before operators notice it. In practice, first-piece inspection, in-process gauging, and documented surface checks remain essential. Dimensional data should be reviewed against drawing tolerances, ASTM requirements, and the validated cleaning process. A bright surface can still hide contamination. That assumption deserves scrutiny.

Why Choose Swiss Turning Services for Titanium Bone Screws?

Titanium bone screws require high strength, corrosion resistance, biocompatibility, and precise thread geometry. The chart compares the minimum specified tensile and yield strength of commonly used implant-grade titanium materials. Swiss turning is well suited to producing small-diameter screws with consistent dimensions, clean thread profiles, and repeatable tolerances.

Values are representative minimum mechanical requirements in MPa from commonly referenced ASTM implant-material specifications. Actual properties vary with product form, heat treatment, and manufacturing condition.

Swiss Turning: How the Precision Machining Process Works

Swiss turning is well suited to titanium bone screws because it supports accurate machining of small, slender components. The process begins with titanium bar stock passing through a guide bushing. The bushing stays close to the cutting area. This reduces deflection during turning. A sliding headstock moves the material while tools shape the screw profile. Precise timing controls threads, diameter, and undercuts.

The cutting tools follow programmed paths around the rotating bar. Live tooling can create drive recesses or cross features without moving the part between machines. That matters. Fewer setups can reduce alignment errors. Titanium generates heat and may resist cutting, so machinists monitor speed, feed rate, and coolant flow carefully. Poor control can cause tool wear, burrs, or a rough thread surface.

After machining, each screw needs close inspection. Technicians may check thread dimensions, head geometry, surface condition, and overall length with calibrated equipment. Optical systems can inspect small features that are difficult to measure by touch. Lot records and material certificates support traceability. No process is flawless. Even a well-designed Swiss turning cycle may need adjustment after tool wear or material variation appears. Experienced teams review these findings and refine the process without losing dimensional control.

Why Titanium Bone Screws Require Swiss-Type Machining

Why Choose Swiss Turning Services for Titanium Bone Screws?

Why Titanium Bone Screws Require Swiss-Type Machining

Titanium bone screws demand controlled cutting, not simply sharp tools. Titanium conducts heat poorly, at roughly 7 W/m·K, according to ASM International data. Heat therefore remains near the cutting edge. The material also springs back and can harden during unstable cutting. Small errors may damage threads, recesses, or the screw’s seating surface.

Swiss-type machining supports this geometry. A guide bushing holds the slender blank close to the cutting zone. That reduces deflection during thread production and cross-hole drilling. Live tooling can complete several features in one setup. Fewer setups often mean fewer alignment risks. It is a practical advantage.

The details matter. Stable coolant flow helps control heat. Sharp, dedicated tools reduce burr formation. Measured thread pitch and surface finish support reliable assembly. ASTM F136 titanium alloy is widely specified for surgical implants, while ISO 5832-3 defines requirements for wrought titanium alloy. These standards guide material control, but machining still determines the final surface.

Grand View Research reported in 2024 that the orthopedic implants market is expected to grow at about 4% annually through 2030. That growth increases pressure for repeatable production and traceable inspection. However, Swiss turning is not magic. Tool wear can still alter a tiny thread profile. Experienced manufacturers must inspect first-off parts, monitor runout, and review process data continuously. Even good processes need questioning.

Key Benefits of Swiss Turning for Medical Screw Production

Why Choose Swiss Turning Services for Titanium Bone Screws?

Swiss turning supports precise, repeatable production of titanium bone screws with complex threads, slots, and small diameters. The guide bushing holds long, slender parts close to the cutting tool. This reduces deflection and helps control thread geometry. Live tooling can also machine drive recesses and cross-holes in one setup. Fewer setups usually mean fewer alignment errors.

Consistency matters in orthopedic production. Grand View Research valued the global orthopedic implants market at approximately US$47.4 billion in 2023. Its report forecasts continued growth through 2030.

That growth increases pressure on manufacturers to produce reliable components at controlled costs. Swiss turning can support this need through automated bar feeding, in-process checks, and documented inspection data. Titanium alloys remain challenging, however. They generate heat and can react poorly to careless cutting conditions. Tool wear must be monitored.

Small details matter.

Experienced machinists typically adjust cutting speed, coolant delivery, and tool engagement for each titanium grade. A stable process can improve surface quality around threads and bearing areas. It may also reduce burrs that require secondary finishing.

ISO 13485-based quality systems emphasize traceability and controlled production records. Those records help connect material certificates, machine settings, inspection results, and operator reviews.

Swiss turning is not magic. A poorly designed thread can still fail inspection. An overly aggressive tolerance can increase scrap without improving clinical performance. Engineers should review anatomy, fixation loads, cleaning requirements, and manufacturing limits together. That practical discussion often prevents expensive revisions later.

Quality Control, Compliance, and Supplier Selection Criteria

Swiss turning can produce titanium bone screws with clean threads, stable diameters, and repeatable features. That matters when a screw must fit a narrow surgical instrument. However, precision alone is not enough. Supplier selection should begin with documented process control, not attractive samples.

ISO’s 2023 Survey recorded more than 30,000 ISO 13485 certificates worldwide. Certification supports confidence, but it does not replace technical review. Ask for machining validation, inspection plans, material certificates, and complete batch traceability. A capable supplier should verify titanium grade, bar identity, thread geometry, surface condition, and critical dimensions. Coordinate measuring machines, optical inspection, and calibrated gauges provide stronger evidence than visual checks. The 2024 MedTech Europe industry report describes a European market exceeding €170 billion, with about 38,000 companies. This scale increases choice, but also makes supplier comparison less simple.

Tips: Request a sample inspection report before approval. Check measurement uncertainty. Review nonconformance handling and corrective-action records. Confirm whether cleaning, passivation, and packaging controls are performed internally or outsourced. Ask how tool wear is monitored during long production runs. Small omissions can become expensive. One uncomfortable point remains: an audit can look excellent while daily discipline quietly weakens. Recheck performance through periodic audits, capability studies, and trend reviews. Compliance should be demonstrated repeatedly, not promised once.

Why Choose Swiss Turning Services for Titanium Bone Screws? — Quality Control, Compliance, and Supplier Selection Criteria

Procurement reference table for evaluating Swiss precision-turning suppliers of titanium bone screws. Numerical targets are example purchasing criteria and should be confirmed through design validation, risk analysis, and applicable regulatory requirements.
Evaluation Dimension Recommended Benchmark or Requirement Typical Verification Evidence Relevance to Titanium Bone Screws
Material Grade Use implant-grade titanium such as Ti-6Al-4V ELI or commercially pure titanium, selected according to the screw design and intended application. Material certificate with heat or lot number, chemical composition, mechanical properties, and full traceability. Material grade affects strength, fatigue performance, corrosion resistance, biocompatibility, and compatibility with sterilization processes.
Material Standards Specify applicable standards such as ASTM F136 for wrought Ti-6Al-4V ELI, ASTM F67 for unalloyed titanium, or ISO 5832-3 where applicable. Certificate of conformity, incoming inspection records, and documented material acceptance criteria. Standardized material requirements reduce variation between production lots and support regulatory submissions.
Dimensional Accuracy Define tolerances by drawing and risk assessment; precision-turned features may commonly use approximately ±0.01 to ±0.05 mm, depending on geometry and function. Coordinate-measuring-machine reports, calibrated gauges, first-article inspection, and capability studies for critical dimensions. Accurate threads, drive recesses, undercuts, and screw heads support insertion performance and implant compatibility.
Thread Profile and Pitch Control pitch, major diameter, minor diameter, thread form, crest condition, and thread runout according to the approved drawing. Optical measurement, thread gauges, functional mating tests, and inspection of thread flanks and crests. Thread geometry directly influences insertion torque, pull-out behavior, bone engagement, and mating with instruments or plates.
Surface Finish Set drawing-specific roughness limits; a common controlled range for machined functional areas may be Ra 0.8–1.6 µm, subject to the validated design. Calibrated profilometer results, visual inspection under defined lighting, and records for polishing, cleaning, or passivation. Surface condition affects debris generation, cleanability, corrosion behavior, tissue interaction, and fatigue initiation sites.
Burr and Edge Control No loose burrs, sharp unintended edges, torn material, or machining damage on threads, drive recesses, and bone-contacting surfaces. Defined visual standard, magnified inspection, tactile inspection where appropriate, and documented deburring validation. Effective edge control helps limit particulate contamination and protects handling, insertion, and tissue-contact performance.
Mechanical Testing Validate insertion torque, removal torque, torsional strength, axial pull-out, and fatigue performance according to the product risk profile and applicable test methods. Validated test protocols, raw data, sample traceability, acceptance criteria, and signed test reports. Mechanical testing confirms that dimensional control and material selection translate into safe clinical performance.
Quality Management System Prefer a supplier operating an audited medical-device quality system aligned with ISO 13485:2016 and supported by documented process controls. Current certificate, audit reports, nonconformance records, corrective-action history, and change-control procedure. A medical-device QMS provides controlled design transfer, production, inspection, traceability, and complaint-support processes.
Risk Management Maintain risk-management documentation consistent with ISO 14971, including hazards related to breakage, particulate matter, incorrect dimensions, and contamination. Risk-management file inputs, process FMEA, control plan, inspection plan, and evidence that production risks are linked to acceptance criteria. Risk-based controls help prioritize critical features rather than relying only on general visual inspection.
Biological Safety Support Provide material and process information to support biological evaluation under ISO 10993, as applicable to the finished device and contact duration. Material composition, cleaning-agent information, residual analysis, surface-treatment records, and supplier declarations. Manufacturing residues and surface treatments can affect the biological safety assessment of an implant.
Cleaning and Contamination Control Use a validated cleaning process with controlled water quality, detergents, handling, packaging, and particulate limits appropriate for the device. Cleaning validation, residual testing, particle monitoring, environmental procedures, and packaging-integrity records. Small threaded components can retain chips, oils, and residues if cleaning and handling controls are inadequate.
Regulatory Compliance Confirm the supplier can support applicable Swiss MedDO and/or EU MDR obligations, depending on the legal manufacturer, device classification, and market. Regulatory responsibilities matrix, technical-documentation inputs, declarations, certificates, and change-notification commitments. Clear allocation of responsibilities prevents gaps between the component supplier, legal manufacturer, and regulatory submission.
Process Validation Validate special or outcome-dependent processes such as thread rolling, heat treatment, surface treatment, cleaning, passivation, and packaging where applicable. Validation protocols, approved process parameters, revalidation triggers, and objective evidence of repeatability. Validated processes reduce the likelihood that acceptable-looking parts will have hidden mechanical or contamination-related defects.
Inspection and Measurement System Use calibrated equipment with documented measurement uncertainty and gauge capability appropriate to the tolerance being inspected. Calibration certificates, measurement-system-analysis studies, inspection instructions, and equipment-maintenance records. Reliable measurement is essential when small dimensional differences affect fit, insertion, or mechanical performance.
Traceability Maintain traceability from raw-material heat or lot through machining batch, inspection results, cleaning, packaging, and shipment. Batch records, traveler documents, certificates, labeling records, and electronic or controlled paper genealogy. Traceability supports efficient investigations, targeted containment, and regulatory reporting when required.
Supplier Change Control Require advance notification and approval for changes to material source, tooling, CNC program, process parameters, subcontractors, inspection methods, or packaging. Formal change-control procedure, change-impact assessment, requalification plan, and retained approval records. Uncontrolled changes can alter thread accuracy, surface condition, fatigue strength, or cleanliness without obvious visual differences.
Capacity and Delivery Reliability Assess available Swiss-type turning capacity, approved subcontractor controls, lead-time consistency, safety stock options, and business-continuity planning. Capacity plan, historical on-time-delivery data, contingency plan, production schedule, and escalation contacts. Stable supply is important for surgical-device production, especially when screws are matched to instruments or implant systems.
Supplier Selection Scorecard Suggested weighting: quality and compliance 30%, technical capability 25%, traceability and documentation 15%, delivery reliability 15%, total cost 10%, communication and support 5%. Completed audit checklist, weighted supplier score, documented corrective actions, sample approval, and management review. A weighted scorecard prevents low price or short lead time from outweighing patient-safety and regulatory risks.
Reference framework: ISO 13485:2016 for medical-device quality management, ISO 14971 for medical-device risk management, ISO 10993 for biological evaluation, ASTM F136 or ASTM F67 for applicable titanium implant materials, and the applicable requirements of Swiss or European medical-device legislation.
PFC CONTROLS
1638 NW 108TH AVE. MIAMI, FL 33172
Sales: (305) 593-0227
Tech: (305) 546-3965

Copyright, All rights reserved
Back to content